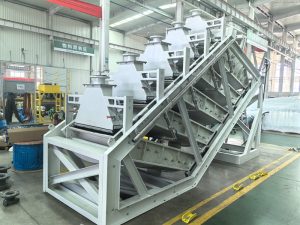
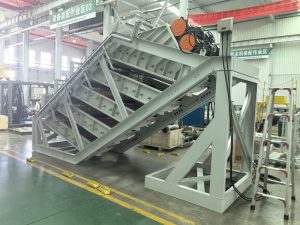
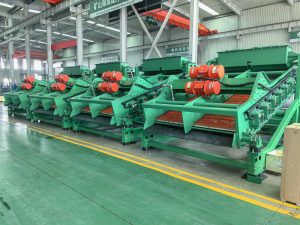
GN Solids Control has delivered 2 sets of GNFG1440 high frequency fine screens to an overseas mining operator, expanding GN’s mining processing product portfolio built on decades proven shale shaker vibration screen technology GN separation.
Mining projects face persistent pain points in fine‑particle handling: conventional vibrating screens frequently suffer mesh blinding, poor classification accuracy and unstable throughput when processing wet fine ore, tailings slurry and coal slurry. GNFG1440 is purpose‑engineered to solve these bottlenecks. Adopting two‑degree‑of‑freedom resonance vibration principle and dual imported vibration motors, this unit delivers stable linear motion with 2‑3 mm amplitude, promoting orderly particle stratification and drastically reducing screen‑blocking risksGN Solids. It offers big size effective screening area, balancing large throughput and precise fine‑size classification performance.
Drawing manufacturing standards from GN shale shaker production, the whole screen box uses high‑strength steel and undergoes stress‑relief heat‑treatment after welding to resist deformation under continuous heavy‑duty cyclic vibrationGN Separat…. The screen deck angle can be mechanically adjusted on‑site to adapt variable ore moisture and feed characteristics. Wear‑resistant polyurethane screen panels with 28‑45 % open area are fitted as standard; normal service life can reach more than six months to cut spare‑part replacement costs. Wetted surfaces are available with polyurea anti‑abrasion coating for corrosive mineral slurry conditions.
Beyond GNFG1440 fine screens, GN provides one‑stop separation solutions including multi‑deck fine screens, decanter centrifuges, skid‑mounted slurry‑treatment packages and full ranges of interchangeable screen panels. Supported by mature FAT factory testing, pre‑sales process simulation and global after‑sales service network, GN transfers reliable vibration‑separation know‑how originally developed for oil‑gas solids‑control into mineral‑processing sectors.
This shipment marks another milestone for GN in global mining market, delivering cost‑effective and durable screening equipment for fine‑ore classification, tailings recovery and slurry dewatering requirements.


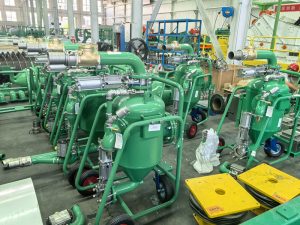
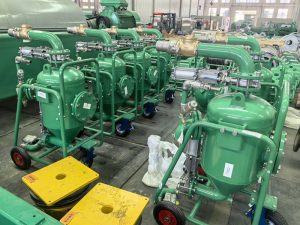
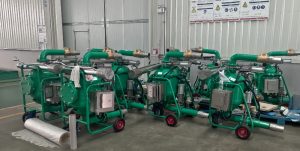
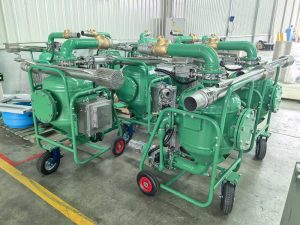
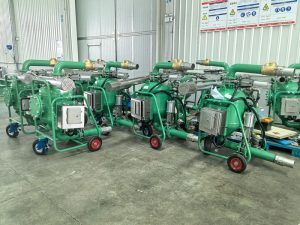
We are pleased to share that a batch of our GN series pneumatic sludge vacuum transfer pumps has completed factory assembly and testing, ready for shipment to our overseas customer. Also called solids transfer pump, this air-powered unit is a proven workhorse for heavy-duty solids and sludge handling in oilfield, HDD tunneling and waste treatment projects.
Thanks to its special structural design, this vacuum pump works reliably under tough site conditions with minimal maintenance. It can transfer high-gravity, high-density slurries, with solids content up to 80%. We offer three models: GNSP-10B, GNSP-20B and GNSP-40B, covering a flow range from 10 m³/h to 40 m³/h. It features strong suction capacity up to 50 m and a maximum discharge distance of 1000 m, and can pass solid particles as large as 75 mm, greatly reducing clogging risks.
Driven entirely by compressed air, the pump requires no electric motor on site. This design delivers excellent safety advantages for humid, explosive or power-limited job sites. Mounted on a wheeled mobile frame, the pump can be quickly moved between mud pits, shale shakers, centrifuges and waste tanks without extra lifting equipment. The quick-opening access cover simplifies inspection and internal cleaning to cut downtime.
This pump supports diverse applications: transferring waste mud and solids from solids control equipment, cleaning waste pits, removing tank bottom oil sludge, recovering hazardous waste, and handling sand, diatomaceous earth and animal waste.
This pump boasts outstanding conveying capacity and anti-clogging performance. It can stably transport high-density sludge, oil sludge, solid-liquid mixtures and granular materials, with the solid content of conveying materials up to 80%. Supporting ultra-long-distance conveying and strong self-priming work, it can smoothly pass large-particle impurities, effectively solving the common problems of blockage, shutdown and difficult material suction of traditional sludge pumps.
In terms of operation and maintenance, the mobile trolley design realizes flexible overall movement, allowing free switching between multiple working areas without large hoisting equipment. Equipped with quick-opening inspection structure and high-quality sealing accessories, the equipment is convenient for daily cleaning and maintenance, greatly reducing later operation cost and equipment failure rate.
All our pneumatic sludge transfer pumps are manufactured in strict accordance with international industry standards, with pressure-resistant and wear-resistant structural design, ensuring long-term stable operation under high-load working conditions. Adhering to reliable quality and professional service,GN always provides cost-effective solid control and material conveying equipment for global customers.


When drilling contractors focus on well‑drilling efficiency, wastewater generated during mud‑tank cleaning is often an overlooked operational headache, especially for remote African oilfields. Limited infrastructure, scarce freshwater resources and tightening local environmental rules make off‑site waste haul‑away expensive and impractical.
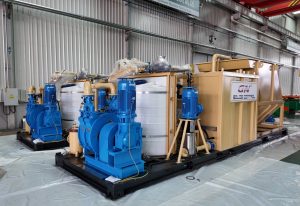
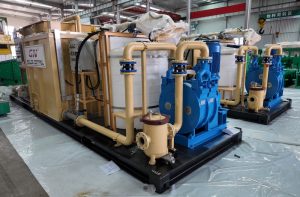
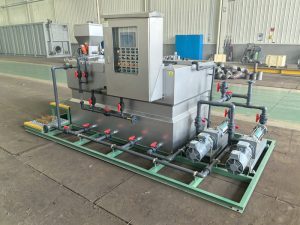
GN Solids Control has recently completed and shipped four custom‑built skid‑mounted drilling mud tank‑cleaning wastewater treatment units for an African oil‑gas client, delivering a turn‑key solution targeting this exact pain point.
This integrated system consists of feeding pump, pre‑separation tank, chemical dosing package, decanter centrifuge, clean water tank, control cabinet and all connecting pipelines. All core components are mounted on heavy‑duty skids for easy transportation between scattered well sites. The whole unit adopts continuous treatment process: oily wastewater from mud tank washing first enters pre‑separation compartment to remove large solids. After chemical conditioning, the fluid flows into the GNLW decanter centrifuge, which efficiently separates fine solids and free oil from water.

The system implements mature three‑phase separation technology to handle tank‑cleaning sewage mixed with oil, fine drilling solids and residual mud. It separates oil phase, solid sediments and reusable water simultaneously. Recovered water can be circulated back for repeated site usage, drastically cutting fresh‑water consumption. Dewatered solid residues are ready for compliant haul‑off, lowering hazardous‑waste transport volumes and overall operational expenditure.
Each unit is pre‑optimized for harsh African field conditions: high temperature, heavy dust and unstable on‑site power supply. Explosion‑proof electrical options are available for hazardous zone applications. It can connect seamlessly with customers’ existing mud‑tank cleaning workflow without major modification to current facilities.
GN provides full after‑sales support including operation manuals, remote technical guidance and spare parts package. Besides mud tank cleaning wastewater units, we also manufacture shale shakers, mud cleaners, decanter centrifuges and complete solids control systems for global oilfield clients.
If you are struggling with mud‑tank‑cleaning oily wastewater disposal at your site, feel free to contact GN Solids Control for a customized budgetary proposal.

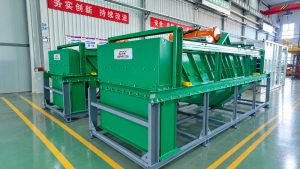
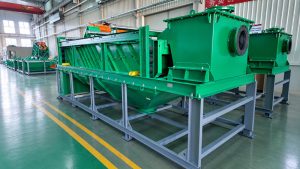
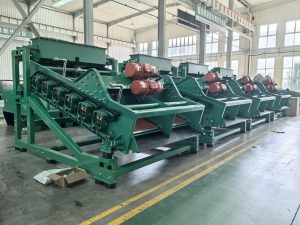
GN Solids Control is pleased to announce the delivery of a 5-deck Stack Vibrating Screen to an overseas customer. As a self-developed fine screening equipment, GN Stack Vibrating Screen is mainly designed for wet screening, classification and dehydration of fine-grained materials in mineral processing, coal preparation and other industries.

The GN Stack Vibrating Screen can be configured with 2 to 5 screening decks according to different site requirements. Driven by dual vibration motors and designed based on the two-degree-of-freedom resonance principle, the screen box performs stable linear motion with high screening efficiency and low energy consumption.
Compared with conventional vibrating screens, the multi-deck structure provides a larger processing capacity per unit area while reducing footprint, dynamic load and maintenance requirements. The equipment adopts polyurethane screen mesh, featuring high elasticity, a 28–45% opening rate and an average service life of more than six months. Pull-bolt screen fixing components ensure convenient installation and reliable fastening.

For demanding working conditions, the screen surface receives sandblasting and heavy-duty anti-corrosion coating, while material-contact areas are protected with a wear-resistant polyurea resin layer. The modular feeding box, internal buffer plates and material distribution plate help reduce material impact, improve feeding uniformity and extend screen service life.
GN continues to develop efficient and reliable screening solutions for customers worldwide.


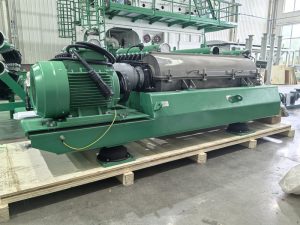
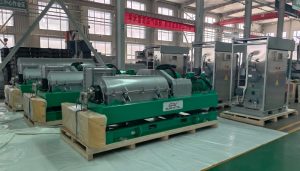
GN Solids Control has recently completed a batch delivery of GN Solids Vacuum Pumps and Decanter Centrifuges to a customer in the Middle East. The equipment will be used for efficient solids, slurry, and sludge transfer as well as industrial solid-liquid separation applications.
The GN Solids Vacuum Pump, also known as a sludge vacuum pump, is a vacuum loading solids transfer pump fully powered by compressed air. It can load materials under a vacuum of up to 25″ Hg and deliver them over distances exceeding 500 meters. Available models include capacities of 10, 20, and 40 m³/h. The compact and robust design allows the pump to handle solids, powder, slurry, sludge, and other challenging materials. Since it requires no electrical power, it is also suitable for applications where explosion-proof equipment is required.

The GN Decanter Centrifuge is a horizontal screw centrifuge widely used for industrial solid-liquid separation. Depending on material characteristics, GN offers dewatering, separation, and clarification models, while centripetal pump technology enables three-phase liquid-liquid-solid separation.

GN combines quality materials, precision CNC machining, and high-speed dynamic balancing technology to ensure reliable and stable centrifuge performance. The successful batch delivery demonstrates GN‘s capability to provide reliable solids handling and separation solutions for customers across the Middle East.


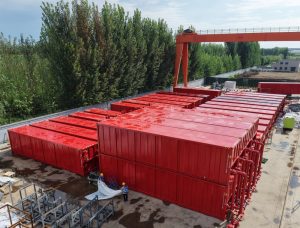
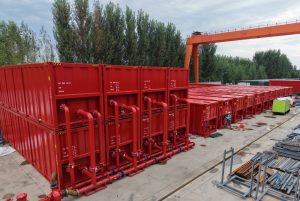
GN Solids Control has recently supplied a 14,000BBL Fast-Moving Mud Station to a professional drilling fluid company, providing a flexible and efficient solution for large-scale drilling operations.

Designed in accordance with API-650, the mud station is engineered to meet the demanding requirements of drilling fluid storage and handling. Each mud tank is designed in a 40-ft high cube container configuration, with a capacity of 440BBL, making the system convenient for transportation, installation and relocation between different drilling sites.
A key feature of this mud station is its CSC container certification, which supports safe and efficient transportation while reducing the complexity of logistics. The containerized design allows the equipment to be quickly mobilized and deployed, making it particularly suitable for drilling projects where site conditions and equipment locations may change frequently.

To maximize the utilization of limited site space, the mud tanks are also designed for two-level stacking. This configuration significantly reduces the overall footprint while maintaining the required storage capacity, offering drilling fluid companies greater flexibility in site layout.
With its large storage capacity, containerized structure, certified transportation design and space-saving configuration, the GN Solids Control 14,000BBL Fast-Moving Mud Station provides a reliable solution for modern drilling fluid management and rapid deployment requirements.